Surgical Instrument Manufacturer Selecting Bone cutting forceps is a clinical, technical, and procurement decision. The right instrument must match bone density, surgical access, hand strength, and sterilization routines. A forceps that feels smooth during inspection may still cause fatigue after repeated procedures. Small details matter, including jaw alignment, hinge resistance, handle texture, and the visibility of the cutting edge.
The World Health Organization reports that approximately 1.71 billion people live with musculoskeletal conditions worldwide. This broad burden supports continued demand for dependable orthopedic and surgical instruments. However, global buyers should not treat market demand as proof of product quality. Manufacturer experience, documented material specifications, traceability, and validated quality systems deserve closer attention. ISO 13485 certification can indicate a structured medical-device quality process, but certification alone does not guarantee superior cutting performance.
Look closely.
This guide presents seven practical evaluation points for Bone cutting forceps, including material selection, jaw geometry, ergonomics, corrosion resistance, cleaning compatibility, supplier documentation, and regulatory readiness. FDA guidance on reusable medical devices emphasizes clear reprocessing instructions and design considerations that support effective cleaning. Those requirements are especially important when instruments contain tight hinges or textured surfaces. Buyers should also compare test evidence, warranty terms, sample performance, and feedback from qualified clinical users. No checklist is flawless. A forceps may pass visual inspection yet disappoint in real operating conditions. Careful sampling, controlled trials, and honest post-purchase review remain essential for safer, more reliable sourcing across international markets.
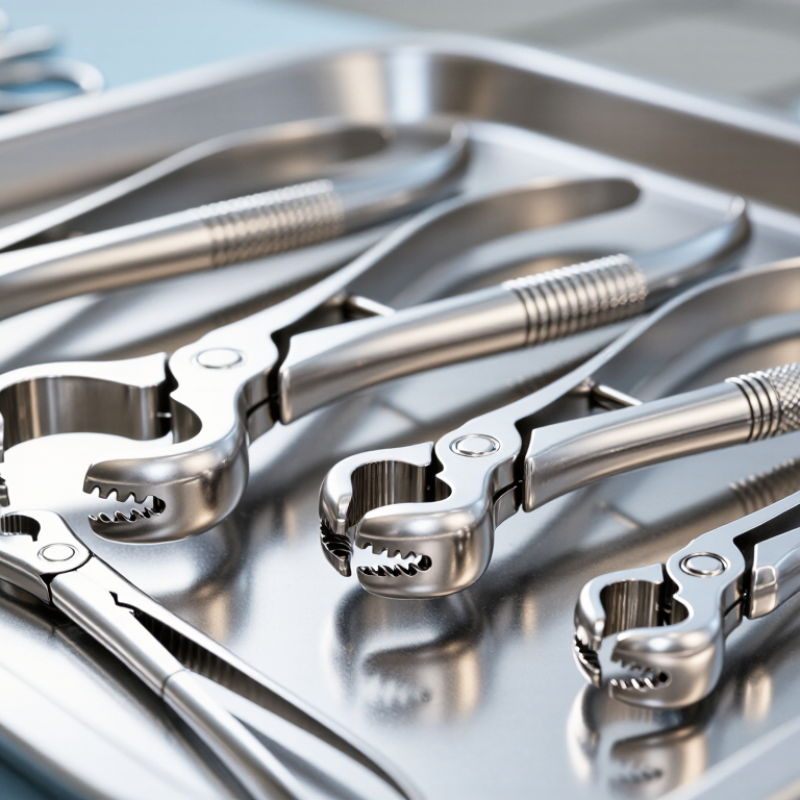
Choosing bone cutting forceps should begin with the task, not the catalog price. A tool for trimming small bone fragments needs different jaws from one used on dense cortical bone. Clarify the procedure, access angle, and expected cutting frequency before comparing models. A narrow, angled jaw can improve visibility in confined areas. A broader jaw may provide better stability during heavier cuts.
Jaw pattern directly affects control and tissue protection. Consider straight, curved, rongeur, or side-cutting designs according to the working direction. Check the cutting diameter against the bone size. Oversized jaws may crush instead of cut cleanly. Undersized jaws can require repeated pressure and increase hand fatigue. Measure typical specimens whenever possible. Guesswork is expensive.
Force requirements also deserve practical testing. A sharp edge should cut with steady pressure, not sudden squeezing. Ask for material data, jaw alignment records, and repeated-cycle testing. Inspect the hinge for smooth movement and unwanted lateral play. In one evaluation, a compact instrument looked efficient, but its short handles demanded excessive grip force. That detail was nearly missed. It changed the selection.
Do not rely on one specification sheet. Test samples with realistic loads and trained users. Record hand comfort, cut quality, and maintenance needs. Local clinical rules and procurement standards may also affect acceptance.
7 Tips to Choose Bone Cutting Forceps for Global Buyers
For global buyers, the steel grade deserves more attention than the polished surface. ASTM F899 identifies 420 and 440A as martensitic stainless steel options for surgical instruments. Its chemical tables show 420 with about 12–14% chromium and 440A with about 16–18%. Carbon content differs significantly. This affects hardness, edge retention, and toughness after heat treatment.
Tip one: request the exact ASTM F899 grade, not “surgical stainless steel.” Tip two: verify the mill certificate and heat-treatment records. Tip three: compare hardness after processing. Properly treated 420 often offers better toughness, while 440A can provide stronger edge retention. Tip four: inspect the cutting edges under magnification. Tiny burrs may damage performance. Tip five: check corrosion resistance after cleaning cycles. ISO 7153-1 emphasizes material suitability for surgical instruments, but it does not replace product testing.
The choice is not automatic. A harder 440A jaw may keep its bite longer, yet excessive hardness can increase chipping risk. A 420 jaw may tolerate repeated impact better, but it may lose sharpness sooner. That trade-off matters.
Ask for test conditions. Cleaning chemistry, sterilization temperature, and jaw alignment can change results. ASTM F899 confirms material identity, not complete forceps performance. I would also request cutting-cycle data using a defined bone substitute. One overlooked detail can distort the comparison. Manufacturers sometimes provide impressive hardness figures without explaining the test location or method. That deserves cautious review.
Comparing 420 and 440A Stainless Steel Against ASTM F899 Material Grades
The chart shows the commonly specified carbon and chromium composition ranges for 420 and 440A martensitic stainless steel grades referenced in ASTM F899. Higher chromium generally supports corrosion resistance, while carbon content contributes to achievable hardness after heat treatment. Actual instrument performance depends on heat treatment, microstructure, geometry, surface finish, and cleaning conditions. Buyers should confirm the current specification and mill certificate before purchasing.
Request the exact material designation and verify it against the applicable ASTM F899 revision.
Choose a heat-treated condition that balances edge retention, toughness, and resistance to chipping.
Consider repeated washing, sterilization, moisture, and contact with cleaning chemicals.
Ask for chemical analysis, heat-treatment records, inspection results, and lot traceability.
Jaw profile, alignment, edge angle, and pivot design can affect cutting force as much as steel selection.
A smooth, properly finished surface helps reduce staining, residue retention, and cleaning difficulty.
Test representative samples for cutting performance, corrosion resistance, sterilization durability, and dimensional stability.
7 Tips to Choose Bone Cutting Forceps for Global Buyers?
Edge life should be tested on the material your surgeons actually cut. A sharp edge can lose performance after repeated contact with dense cortical bone. Ask suppliers for cycle-based cutting results, not a single showroom demonstration. A practical test records cutting force, jaw alignment, burr formation, and the number of cycles before performance drops. The result is not always consistent.
Corrosion resistance deserves equal attention. Stainless steel composition alone does not prove long-term reliability. Inspect passivation records, surface roughness, and corrosion testing after cleaning and sterilization. ISO 7153-1 identifies commonly used metallic materials for surgical instruments, while ISO 17665 requires a controlled, validated moist-heat sterilization process. Small staining around hinges can indicate poor cleaning, trapped residue, or surface damage. Do not dismiss it as cosmetic.
For 134°C steam sterilization, confirm the validated exposure time, drying conditions, and maximum load configuration. The CDC’s Guideline for Disinfection and Sterilization reports 132°C for four minutes in a prevacuum cycle, but actual parameters depend on the sterilizer and instrument design. AAMI ST79 also emphasizes written procedures, routine monitoring, and maintenance. Buyers should request sterilization validation data, biological-indicator records, and post-cycle functional tests. Repeated thermal stress may loosen joints or reduce edge precision. A laboratory result is not a guarantee. Test samples in your own cleaning workflow before placing a large order.
Choosing bone cutting forceps requires more than checking jaw shape, handle comfort, or catalog photos. Global buyers should verify the material against ISO 7153-1 requirements for surgical instruments. Ask for the exact stainless-steel grade, heat-treatment details, and corrosion-test evidence. A vague “medical steel” statement is not enough. Inspectors may need traceable mill certificates.
Review the supplier’s ISO 13485 system certificate and its scope. The certificate should cover surgical instruments, not an unrelated product category. Request controlled drawings, inspection records, risk-management files, and production-batch traceability. Check how the supplier controls jaw alignment, cutting edges, surface finish, and repeated sterilization. A forceps may look precise but cut unevenly after several cycles. That detail matters.
For European distribution, examine MDR records, including classification rationale, technical documentation, clinical evaluation, post-market surveillance, and the declaration of conformity. Confirm that the legal manufacturer and authorized representative are clearly identified. Match model numbers across labels, certificates, test reports, and packaging. One missing digit can create costly confusion. Ask for recent audit findings, not only polished certificates. That request can feel uncomfortable, but it reveals system maturity. Also test sample units under realistic handling conditions, including grip pressure and hinge movement. I would not rely on one sample alone; manufacturing variation is easy to underestimate. Keep written answers, revision dates, and approval records before placing a large order.
7 Tips to Choose Bone Cutting Forceps for Global Buyers
Selecting bone cutting forceps requires more than comparing polished photographs. Experienced buyers screen the supplier’s process, records, and response quality. Ask seven practical questions before approving a purchase.
Check one: What is the MOQ, and can it match your forecast? A low MOQ may increase unit cost or reduce production stability. Check two: Is the lead time realistic, including inspection, packaging, and export handling? Request a written schedule, not a hopeful estimate. Check three: Can every batch be traced through lot numbers, material records, and inspection reports? Traceability should reach the finished instrument.
Check four: What material grade and hardness range are specified? Request test evidence when appropriate. Check five: How are cutting edges inspected for alignment, sharpness, and surface damage? Check six: Does the supplier maintain documented quality controls and corrective-action records? Certificates help, but current records reveal more. Check seven: Can the supplier provide samples, drawings, and clear answers without avoiding difficult details?
Inspect the sample under bright light. Move the handles slowly, then examine the jaws for uneven contact. Do not judge durability from one smooth opening. A small sample can hide fatigue issues, and I have learned that attractive finishing is not proof of reliable cutting performance. Confirm packaging protects the hinge and edges during long-distance transport. Also verify market-specific documentation with your quality or regulatory team, because requirements differ by destination.
| Buyer Check | Screening Target | Evidence to Request | Practical Data Point | Warning Sign | Recommended Decision |
|---|---|---|---|---|---|
| 1. Minimum Order Quantity | Buyer-defined Standard models: 10–50 pieces Custom models: 50–200 pieces |
Written quotation showing MOQ by model, size, finish, packaging configuration, and customization level. | Separate standard-stock MOQ from production MOQ. Confirm whether mixed sizes can count toward one order quantity. | One fixed MOQ is quoted without explaining the effect of engraving, private labeling, special jaws, or individual packaging. | Prefer suppliers whose MOQ matches the intended launch volume and allows a small validation order before scale-up. |
| 2. Lead Time and Capacity | Typical planning range Standard repeat order: 2–6 weeks Custom tooling or design: 6–12 weeks |
Production schedule, sample lead time, tooling timeline, stated annual capacity, and shipment-ready date in the quotation. | Ask whether lead time starts after purchase order, deposit, artwork approval, or final sample approval. | Only a shipping time is provided, with no manufacturing or quality-release timeline. | Require a milestone schedule covering order confirmation, production, inspection, release, and dispatch. |
| 3. Product Traceability | Required Lot or batch-level identification from raw material to finished goods. |
Material certificates, heat or melt number records, batch records, inspection reports, and a sample traceability label. | Traceability should connect the instrument, production batch, inspection result, and packing record. | Only a generic certificate is supplied, or the lot number cannot be linked to the delivered instruments. | Approve only when traceability records can be retained and retrieved for the expected product life and complaint period. |
| 4. Material and Corrosion Resistance | Required Documented surgical-instrument material grade and corrosion-control process. |
Material certificate, grade designation, hardness or mechanical test results where relevant, passivation records, and corrosion-test method. | Common stainless-steel surgical instruments require controlled heat treatment, surface finishing, cleaning, and passivation processes; grade alone is not sufficient. | Material is described only as “medical steel” or “premium stainless steel” without a verifiable grade or certificate. | Request independent verification or a pre-shipment sample inspection when the instrument will be reused or sterilized repeatedly. |
| 5. Cutting Performance and Jaw Geometry | Application-specific Performance must match the intended bone type, anatomy, and surgical technique. |
Technical drawing, jaw dimensions, cutting-edge geometry, opening angle, handle length, sample test protocol, and inspection limits. | Do not compare forceps only by overall length. Jaw profile, leverage, cutting-edge alignment, and intended use affect performance. | Supplier provides no drawing, no acceptance criteria, or only describes the tool as “sharp” or “heavy duty.” | Use representative samples for functional evaluation and define measurable acceptance criteria before production. |
| 6. Reprocessing and Packaging Information | Required for reusable devices Clear cleaning, disinfection, inspection, lubrication, sterilization, and storage instructions. |
Instructions for use, reprocessing instructions, packaging specification, shelf-life rationale where applicable, and labeling samples. | Reusable instruments should be evaluated against the buyer’s validated cleaning and sterilization process, including steam sterilization if applicable. | Instructions do not identify whether the instrument is reusable, or packaging and labeling conflict with the product’s intended use. | Complete a compatibility review with the target hospital or distributor before approving the final packaging configuration. |
| 7. Regulatory and Quality-System Evidence | Market-dependent Evidence must match the destination market and product classification. |
Quality-system certificate where applicable, risk-management records, product specifications, declaration or registration documents, complaint procedure, and change-control process. | Relevant references may include ISO 13485 for quality management, ISO 14971 for medical-device risk management, ISO 17664-1 for processing information, and ISO 15223-1 for symbols; applicability depends on the market and device status. | Supplier offers a certificate without scope, validity, issuing body, or product relevance, or refuses to provide controlled technical documents. | Verify certificates directly with the issuing organization or through an accepted conformity-assessment route before commercial launch. |
| 8. Dimensional Consistency | Recommended Controlled dimensions for overall length, jaw width, handle alignment, and opening. |
Approved drawing, tolerance table, first-article inspection report, and sample measurement records. | Use the same measurement method and reference points for every supplier to make quotations comparable. | Dimensions are rounded or copied from a catalogue, with no tolerance information or revision control. | Approve samples only after checking fit, alignment, smooth movement, and consistency across multiple pieces. |
| 9. Quality Inspection and Nonconformance Control | Recommended Defined incoming, in-process, and final inspection controls. |
Inspection plan, sampling method, defect classification, calibration records, corrective-action procedure, and sample final inspection report. | Critical defects may include cracks, misaligned jaws, loose joints, incomplete cutting edges, corrosion, burrs, or incorrect labeling. | Inspection is described as “100% checked” without a checklist, acceptance criteria, or inspection record. | Use a signed quality agreement and, for new suppliers, consider independent pre-shipment inspection. |
| 10. Commercial and Supply Continuity | Recommended Stable pricing, documented changes, and clear after-sales responsibility. |
Quotation validity, payment terms, warranty terms, spare-part policy, change-notification process, and business-continuity information. | Confirm who bears the cost of replacement for nonconforming goods and how design or material changes will be approved. | Price changes are frequent, product revisions are unannounced, or replacement responsibilities are unclear. | Use a written supply agreement with change-control, complaint-response, and corrective-action timelines. |
420 usually offers better toughness after heat treatment. 440A can provide stronger edge retention. Its higher hardness may increase chipping risk. The better choice depends on cutting force and durability needs.
Request the exact steel grade, not simply “surgical stainless steel.” Ask for mill certificates and heat-treatment records. Check whether documents match the delivered batch. A vague certificate is not enough.
Test the jaws on a material similar to dense cortical bone. Record cutting force, jaw alignment, burr formation, and cycle count. A showroom demonstration proves very little. Repeated cycles matter more.
Use magnification to inspect both jaw edges. Look for burrs, uneven contact, chips, or small gaps. Tiny defects can reduce cutting precision. The polished surface may hide them.
Review passivation records, surface roughness, and corrosion-test results. Inspect hinge areas after cleaning and sterilization. Brown staining may indicate residue or surface damage. Do not treat it as merely cosmetic.
Confirm exposure time, drying conditions, and maximum load configuration. Request sterilization validation and routine monitoring records. Check function after repeated cycles. Heat can loosen joints.
Request controlled drawings, inspection records, risk-management files, and batch traceability. The quality system should cover surgical instruments. Review model numbers across labels, certificates, and packaging. One missing digit can create confusion.
No. A material certificate confirms identity, not complete performance. Test samples under realistic grip pressure and hinge movement. Use more than one sample. Manufacturing variation is easy to underestimate.
Choosing the right Bone cutting forceps requires a clear understanding of the intended surgical task. Buyers should evaluate the jaw pattern, cutting diameter, handle design, and required force to ensure efficient and controlled performance. Material selection is equally important: compare 420 and 440A stainless steel with ASTM F899 requirements, then assess edge retention, corrosion resistance, surface finish, and durability after repeated 134°C steam sterilization.
Reliable purchasing also depends on supplier verification. Confirm that material specifications align with ISO 7153-1, while the manufacturer maintains an effective ISO 13485 quality system and complete MDR-related technical records. Before placing an order, review minimum order quantity, production lead time, inspection procedures, traceability, packaging, sterilization compatibility, and after-sales support. These seven checks help global buyers reduce quality risks, improve supply continuity, and select Bone cutting forceps that meet functional, material, and regulatory expectations.